

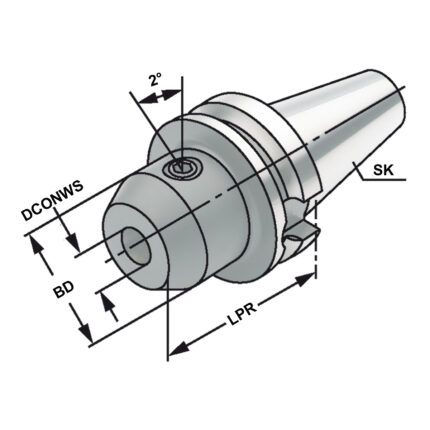
End mill holder Whistle-Notch BT 50 – 20 – 80
Application:
For mounting straight-shank tools and inclined flat according to DIN 1835 form E (Whistle Notch).
Delivery:
With clamping screw and axial adjustment bolt
- All holders are made of forged steel
- Specific, low warpage hardened
- Surface hardened HRC 58~60
- Hardening depth 0,8mm~0,9mm
- Taper angle tolerance < AT 3 according to DIN 2080
- Surface roughness Ra < 0,4 µm
- Tensile strength in the core of min. 800 N/mm? after DIN
- All functional surfaces fine machined


Axial toolholder – form C3 overhead right C3 – 30 x 20
Application:
Mainly for external machining. For face machining.
Precision coolant supply: Improves chip evacuation and decreases the risk for chip jamming, critical factors for successful deep face grooving operations. Effective from low to high coolant pressures.With high precision coolant you get improved
chip breaking, longer tool life, better process security and productivity. Improves chip evacuation and decreases the risk for chip jamming, critical factors for successful deep face grooving operations. Effective from low to high coolant pressures.
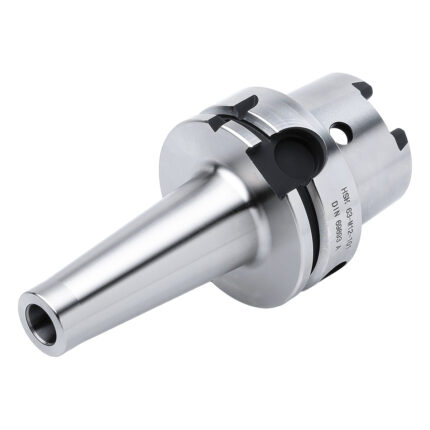
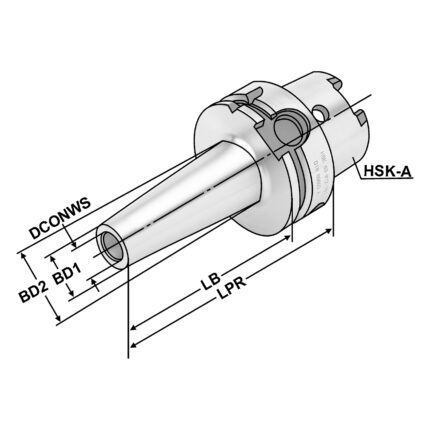
Milling arbors for screw-in cutters HSK 100 – M10 – 79 – LB50
Application:
For mounting screw-in cutters with thread.
- All holders are made of forged steel
- Specific, low warpage hardened
- Surface hardened HRC 58~60
- Hardening depth 0,8mm~0,9mm
- Taper angle tolerance < AT 3 according to DIN 2080
- Surface roughness Ra < 0,4 µm
- Tensile strength in the core of min. 800 N/mm? after DIN
- All functional surfaces fine machined

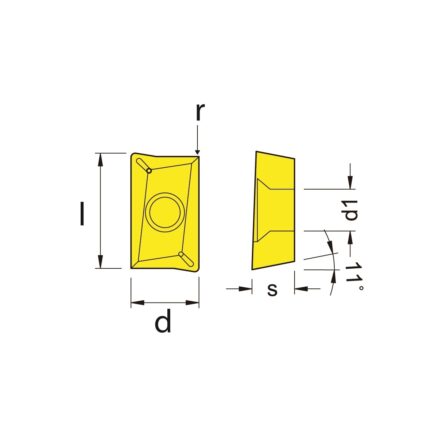


HSS-E spiral flute taps fine thread M8 6×4,9 P=1 DIN 374
Application:
- Thread configuration with a special design, prevents over-feeding, thin thread and pitch diameter oversize.
- Flute geometry with special design, better chip evacuation, prevents chip clogging, improves thread quality
- Excellent performance on various work material: Stainless steel, carbon steel, alloyed steel, tool steel
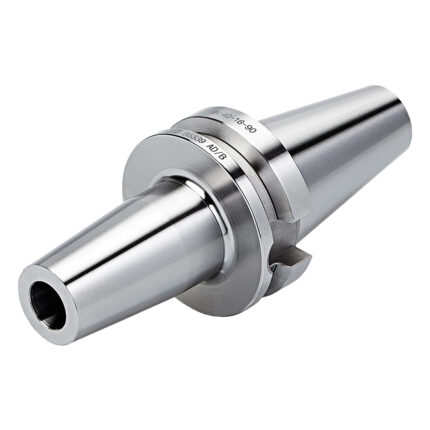
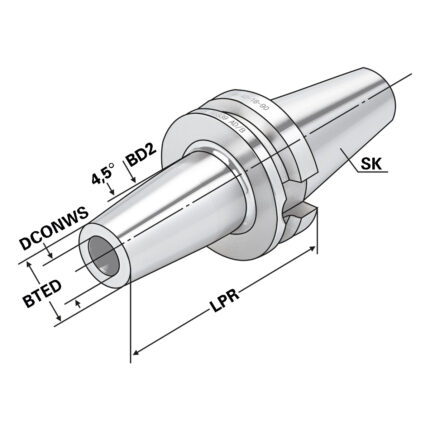
Shrink chuck 4,5° BT 50 – 12 – 160
Application:
For mounting tools with straight shanks.
Note:
Toolholders suitable for induction-, contact- and hot air shrink units. O 3, 4, 5 with h4-tolerance and O 6 O 32 with h6-tolerance
For O 3, 4 and 5 mm only solid carbide tool shanks must be used!
- All holders are made of forged steel
- Specific, low warpage hardened
- Surface hardened HRC 58~60
- Hardening depth 0,8mm~0,9mm
- Taper angle tolerance < AT 3 according to DIN 2080
- Surface roughness Ra < 0,4 µm
- Tensile strength in the core of min. 800 N/mm? after DIN
- All functional surfaces fine machined


Zwischenhulse fur ISO 26623 (PSK) HSK 63 – PSK 32 – 75
Application:
For adaption from HSK-A to PSC (ISO 7388-1 to ISO 26623-1)
Delivery:
Clamping screw
Version:
Adapters HSK / PSK with axial clamping. Ground internally and externally. The internal thread provided for the coolant tube in the PSC toolholder is plugged with the socket-head screw incorporated in the adapter. The clamping screw incorporates a through hole, so the system is suitable for through-coolant feed.
Suitable for tool arbor with polygonal shank (PSC) - ISO 26623-1.


Have questions?
Leave a request
OUR PARTNERS