
PART OF CATALOG

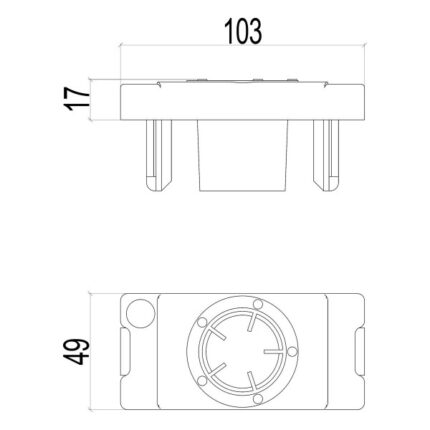
CNC Werkzeugeinsatze | Typ 2 ISO / SK 30
The tool inserts are made of oil-resistant,
break-proof and impact-resistant ABS plastic
and are noted for their tailored inner struts.
The tapered tool holder is thus optimally
centred.
The insert is clicked into our grid system with
a clip and can be moved in steps of 25 mm
without a tool.
Nubs on the top of the inserts.
In this way, no adhesion occurs and the tool
is prevented from attaching itself by vacuum
All tool sizes can be combined


HSS-E spiral flute taps fine thread M10 7×5,5 P=1 DIN 374
Application:
- Thread configuration with a special design, prevents overfeeding, thin thread and pitch diameter oversize.
- Flute geometry with special design, better chip evacuation, prevents chip clogging, improves thread quality
- Excellent performance on various work material: Stainless steel, carbon steel, alloyed steel, tool steel
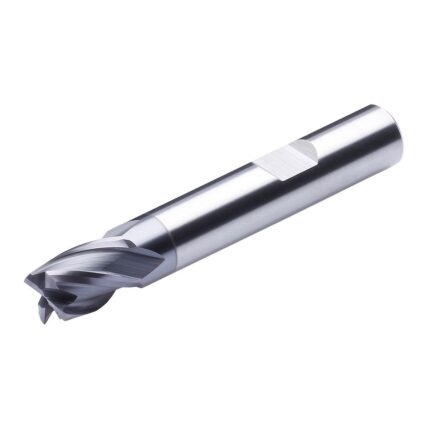

Solid carbide 4 flutes short 3mm 3,0 – 6 AlTiCrN coating

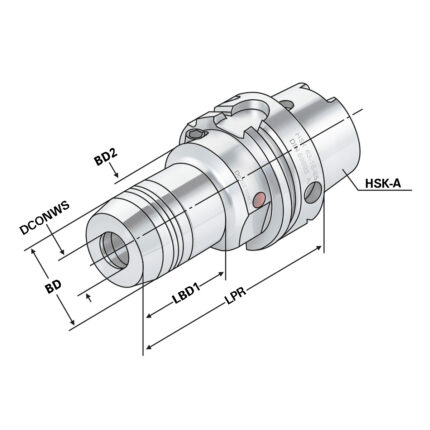
Hydraulic expansion chuck HSK 63 – 10 – 85
Hydraulic expansion chucks, HSK-A 63, New items, Hydraulic chucks special offer 2023, ISO 12164 (HSK-A)
Application:
For mounting straight-shank tools acc. DIN 1835 form A+B+E and DIN 6535 form HA+HB+HE (larger than dia. 20 mm only with reduction sleeve).
Note:
l1 = max. clamping depth l2 = max. length adjustment range
Delivery:
Without wrench
- All holders are made of forged steel
- Specific, low warpage hardened
- Surface hardened HRC 58~60
- Hardening depth 0,8mm~0,9mm
- Taper angle tolerance < AT 3 according to DIN 2080
- Surface roughness Ra < 0,4 µm
- Tensile strength in the core of min. 800 N/mm? after DIN
- All functional surfaces fine machined


Milling arbors for screw-in cutters SK 50 – M12 – 169 – LB150
Application:
For mounting screw-in cutters with thread.
- All holders are made of forged steel
- Specific, low warpage hardened
- Surface hardened HRC 58~60
- Hardening depth 0,8mm~0,9mm
- Taper angle tolerance < AT 3 according to DIN 2080
- Surface roughness Ra < 0,4 µm
- Tensile strength in the core of min. 800 N/mm? after DIN
- All functional surfaces fine machined


Steel boring bar A0810H.SDUC.R07


Collets set ER40 | 472EC | 16-part kit DIN 6499 B (ISO 15488 B) in wooden socket
FREE CONSULTATION
Have questions?
Leave a request
OUR PARTNERS