
PART OF CATALOG
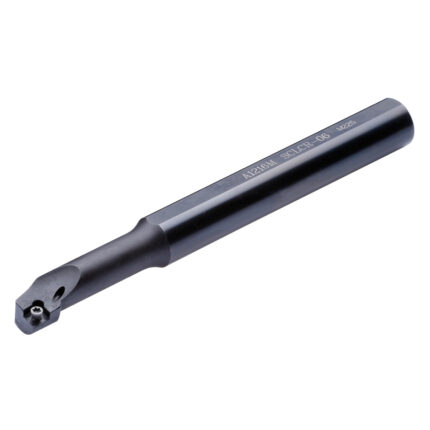
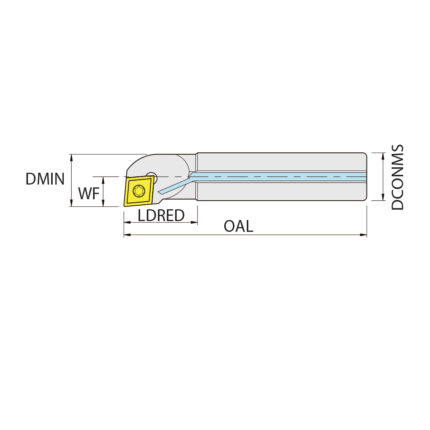
Steel boring bar A1012K.SCLC.R06


Solid carbide 4 flutes short 6mm 6,0 – 6 AlTiCrN coating
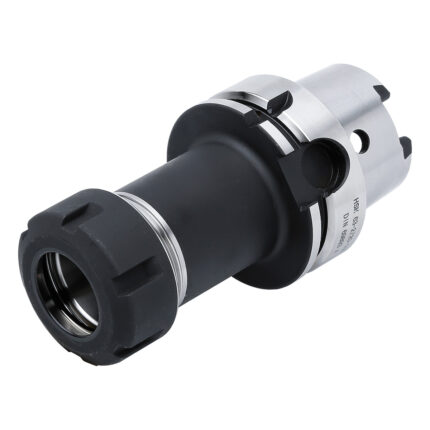
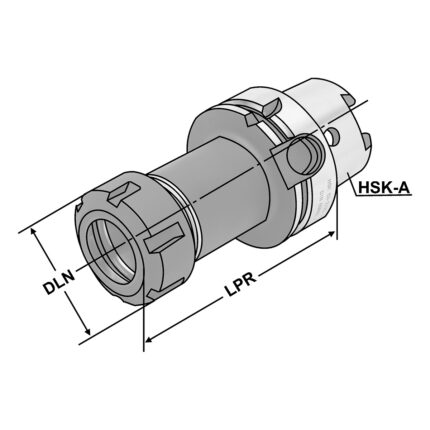
ER-Collet chuck HSK 63 – 2/16 – 160 | ER 25
Application:
For mounting straight-shank tools in collets.
Delivery:
With balanced clamping nut
- All holders are made of forged steel
- Specific, low warpage hardened
- Surface hardened HRC 58~60
- Hardening depth 0,8mm~0,9mm
- Taper angle tolerance < AT 3 according to DIN 2080
- Surface roughness Ra < 0,4 µm
- Tensile strength in the core of min. 800 N/mm? after DIN
- All functional surfaces fine machined


Milling Chuck BT 40 – 25 – 90
Application:
For mounting straight-shank tools.
- All holders are made of forged steel
- Specific, low warpage hardened
- Surface hardened HRC 58~60
- Hardening depth 0,8mm~0,9mm
- Taper angle tolerance < AT 3 according to DIN 2080
- Surface roughness Ra < 0,4 µm
- Tensile strength in the core of min. 800 N/mm? after DIN
- All functional surfaces fine machined
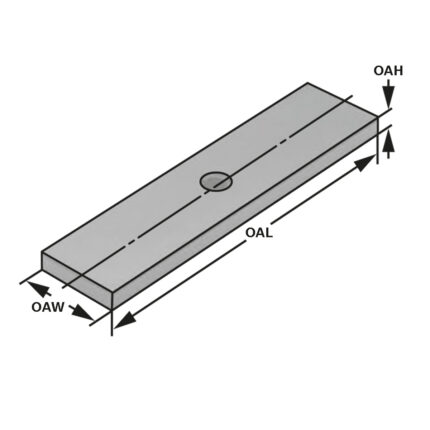
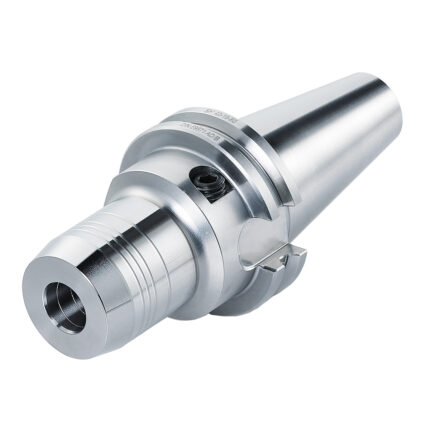

Hydraulic expansion chuck SK 40 – 12 – 77
Application:
For mounting straight-shank tools acc. DIN 1835 form A+B+E and DIN 6535 form HA+HB+HE (larger than dia. 20 mm only with reduction sleeve).
Note:
l1 = max. clamping depth l2 = max. length adjustment range
Without wrench
- All holders are made of forged steel
- Specific, low warpage hardened
- Surface hardened HRC 58~60
- Hardening depth 0,8mm~0,9mm
- Taper angle tolerance < AT 3 according to DIN 2080
- Surface roughness Ra < 0,4 µm
- Tensile strength in the core of min. 800 N/mm? after DIN
- All functional surfaces fine machined


Claw jaws set (Pair) for ATW-50 / ATD-570
Version:
Jaws with grip serrations und fine step for workpieces with max. edge radius 1 mm, clamping depth 2 mm
- For use on vises
- Simple, safe clamping of parallel raw and sawn parts
- Hydraulic or manual clamping
- Positive clamping due to penetration of the hardened claw tips
- High holding forces: increase by a factor of 3 to 5 compared to standard jaws
- Low material loss
- Shortened processing times and reduction of production and unit costs
FREE CONSULTATION
Have questions?
Leave a request
OUR PARTNERS