
PART OF CATALOG


ER-Collet chuck BT 50 – 3/26 – 80 | ER 40
Application:
For mounting straight-shank tools in collets.
Delivery:
With balanced clamping nut
- All holders are made of forged steel
- Specific, low warpage hardened
- Surface hardened HRC 58~60
- Hardening depth 0,8mm~0,9mm
- Taper angle tolerance < AT 3 according to DIN 2080
- Surface roughness Ra < 0,4 µm
- Tensile strength in the core of min. 800 N/mm? after DIN
- All functional surfaces fine machined


ER-Precision collet ER8 | 4004EP | < 5µm | O 4,0 - 3,5


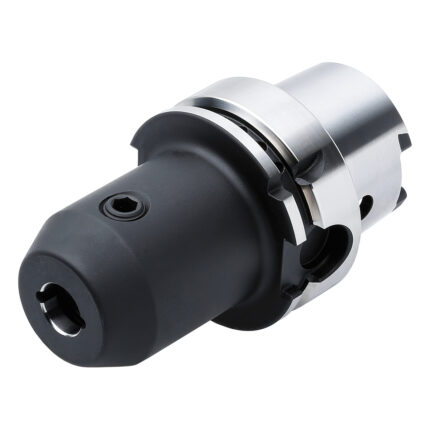

End mill holder Weldon with cooling channels HSK 63 – 12 – 80
Application:
For mounting straight-shank tools with lateral flat according to DIN 1835 form B (Weldon).
Delivery:
With clamping screw and O-ring
- All holders are made of forged steel
- Specific, low warpage hardened
- Surface hardened HRC 58~60
- Hardening depth 0,8mm~0,9mm
- Taper angle tolerance < AT 3 according to DIN 2080
- Surface roughness Ra < 0,4 µm
- Tensile strength in the core of min. 800 N/mm? after DIN
- All functional surfaces fine machined


Swivel base for machine vice HPT 40
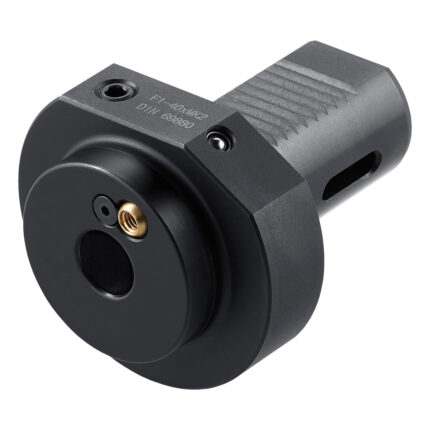

Morse taper adaptor – form F1 F1 – 20 – MK1


Milling arbors for screw-in cutters HSK 100 – M10 – 179 – LB150
Application:
For mounting screw-in cutters with thread.
- All holders are made of forged steel
- Specific, low warpage hardened
- Surface hardened HRC 58~60
- Hardening depth 0,8mm~0,9mm
- Taper angle tolerance < AT 3 according to DIN 2080
- Surface roughness Ra < 0,4 µm
- Tensile strength in the core of min. 800 N/mm? after DIN
- All functional surfaces fine machined


FREE CONSULTATION
Have questions?
Leave a request
OUR PARTNERS