
PART OF CATALOG


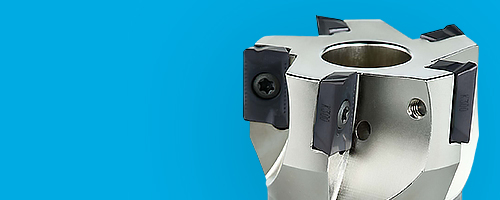
End mill cutter 90° 30mm – 25mm Shank after DIN 1835B


Digital Caliper | 0-150mm for outside grooves / with data output
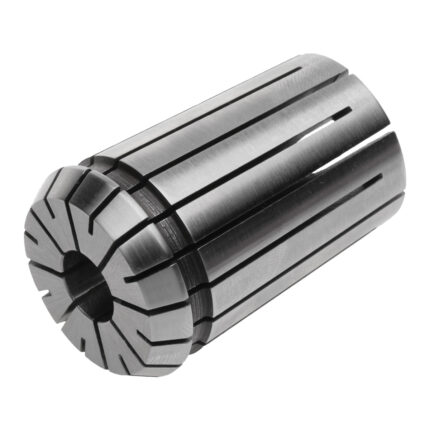
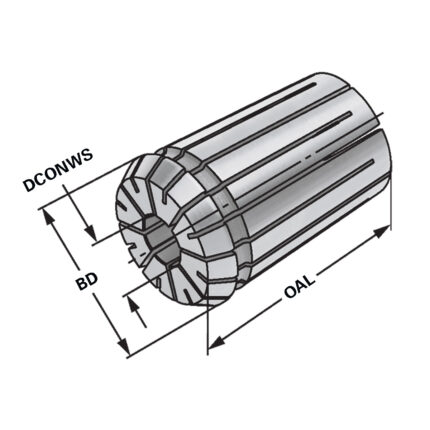
OZ-Collet OZ25 | 462E | < 15µm | O 12 - 11,5


Shell mill holder HSK 100 – 22 – 50
Application:
For mounting milling cutters with transversal groove.
Note:
d = 40/d = 60: For large diameter face mill cutters with four additional threaded holes according to DIN 2079.
SK 30 without coolant exit bores on the end face
Delivery:
With drivers, cross head retaining screw and cylinder head retaining screw for cutters with central coolant. For d = 60 only with four fi xation screws according to DIN 912.
- All holders are made of forged steel
- Specific, low warpage hardened
- Surface hardened HRC 58~60
- Hardening depth 0,8mm~0,9mm
- Taper angle tolerance < AT 3 according to DIN 2080
- Surface roughness Ra < 0,4 µm
- Tensile strength in the core of min. 800 N/mm? after DIN
- All functional surfaces fine machined


OZ-Collet OZ16 | 415E | < 15µm | O 14 - 13,5


Claw jaws set (Pair) for ATW-675 | ATW-689 | MG-60 | AM-C60 | TLD-60
Version:
Jaws with grip serrations und fine step for workpieces with max. edge radius 1 mm, clamping depth 2 mm
- For use on vises
- Simple, safe clamping of parallel raw and sawn parts
- Hydraulic or manual clamping
- Positive clamping due to penetration of the hardened claw tips
- High holding forces: increase by a factor of 3 to 5 compared to standard jaws
- Low material loss
- Shortened processing times and reduction of production and unit costs


FREE CONSULTATION
Have questions?
Leave a request
OUR PARTNERS