

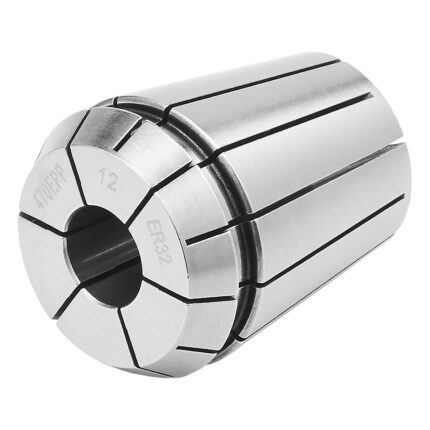

ER-Precision collet ER32 | 470EPP | < 3 µm | O 15,0
Application:
For mounting straight-shank tools in collet chucks ISO 15488 (ex. DIN 6499).
Version:
System concentricity and repetition accuracy 3 µm (3?D, maximum = 50 mm), in conjunction with KEMMLER Precision collet chuck ER".
Suitable for:
KEMMLER Precision collet chuck ER or standard collet chuck Spannfutter ISO 15488 (ex. DIN 6499).
Note:
The collet clamping O range is always up to 0.5 mm less than nominal.
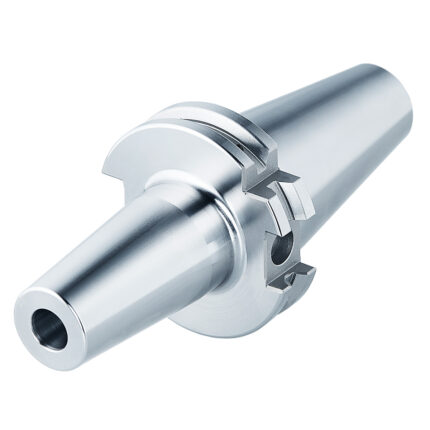
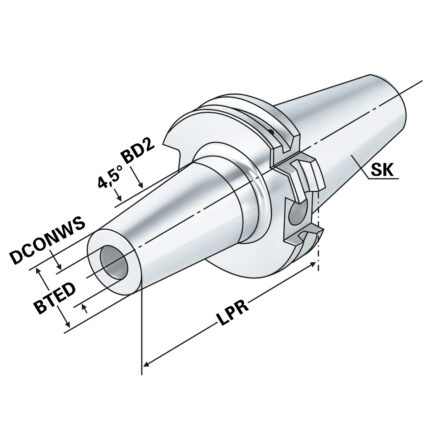
Shrink chuck 4,5° SK 40 – 16 – 160
Application:
For mounting tools with straight shanks.
Note:
Toolholders suitable for induction-, contact- and hot air shrink units. O 3, 4, 5 with h4-tolerance and O 6 O 32 with h6-tolerance9
For O 3, 4 and 5 mm only solid carbide tool shanks must be used!
- All holders are made of forged steel
- Specific, low warpage hardened
- Surface hardened HRC 58~60
- Hardening depth 0,8mm~0,9mm
- Taper angle tolerance < AT 3 according to DIN 2080
- Surface roughness Ra < 0,4 µm
- Tensile strength in the core of min. 800 N/mm? after DIN
- All functional surfaces fine machined


Solid carbide 4 flutes long 12mm 12,0 – 12 AlTiCrN coating


ER-Collet with seal for IC ER25 | 430EH | < 15µm | O 9
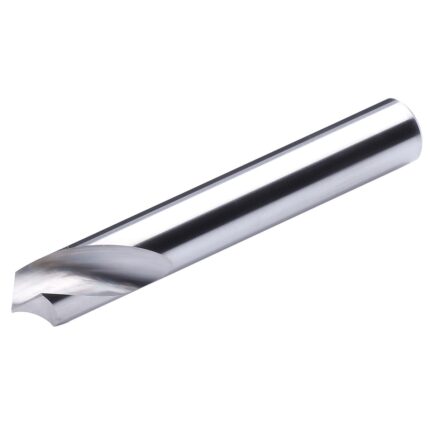

Solid carbide NC spot drill 4mm 120°
Version:
Exactly central ground point. Easy spot drilling and high shape accuracy of the centre hole. Sturdy due to short flutes.
Application:
Point angle 120° for spot drilling and countersinking in one operation when a drill of smaller dia. is used afterwards.
Note:
Use the speed for the actual hole dia. (not generally the speed for the drill outer dia.).


Collet sets 430E (ER25; 15 parts) in wooden box DIN 6499 (ISO 15488)


End mill holder Weldon with cooling channels SK 40 – 14 – 160
Application:
For mounting straight-shank tools with lateral flat according to DIN 1835 form B (Weldon).
Delivery:
With clamping screw and O-ring
- All holders are made of forged steel
- Specific, low warpage hardened
- Surface hardened HRC 58~60
- Hardening depth 0,8mm~0,9mm
- Taper angle tolerance < AT 3 according to DIN 2080
- Surface roughness Ra < 0,4 µm
- Tensile strength in the core of min. 800 N/mm? after DIN
- All functional surfaces fine machined
Have questions?
Leave a request
OUR PARTNERS