
PART OF CATALOG

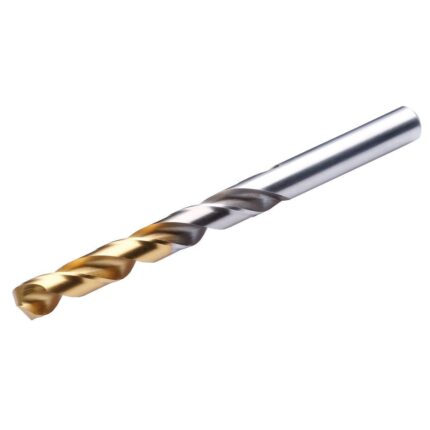

HSSE twist drill 135° 12,1 mm DIN 338 | TIN coating


Solid carbide ball nose end mill 2 flutes long 14m R7,0 – 14 AlTiCrN coating
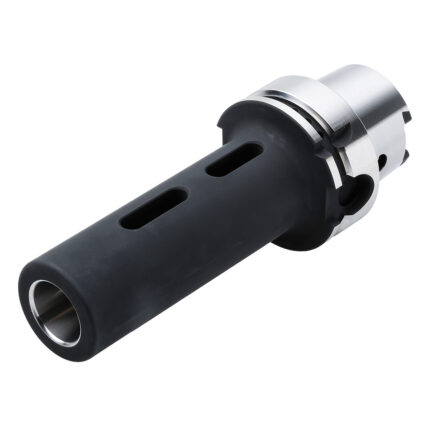

Morse taper adaptor HSK 100 – 3 – 150
Application:
For mounting tools with Morse taper shank and tang according to DIN 228-1 form B.
- All holders are made of forged steel
- Specific, low warpage hardened
- Surface hardened HRC 58~60
- Hardening depth 0,8mm~0,9mm
- Taper angle tolerance < AT 3 according to DIN 2080
- Surface roughness Ra < 0,4 µm
- Tensile strength in the core of min. 800 N/mm? after DIN
- All functional surfaces fine machined
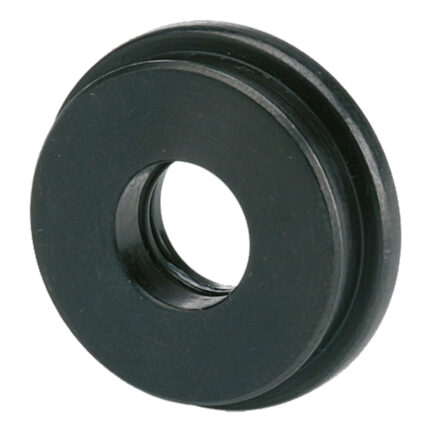
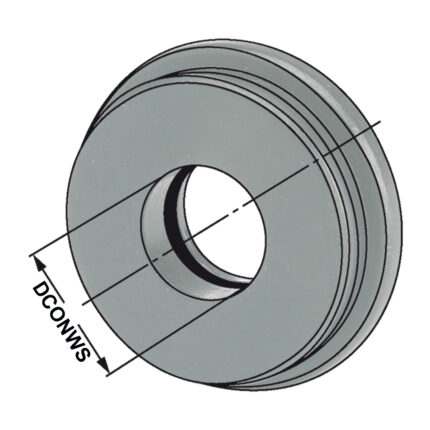
Sealing disc | ER 16 DCONWS = 2,0
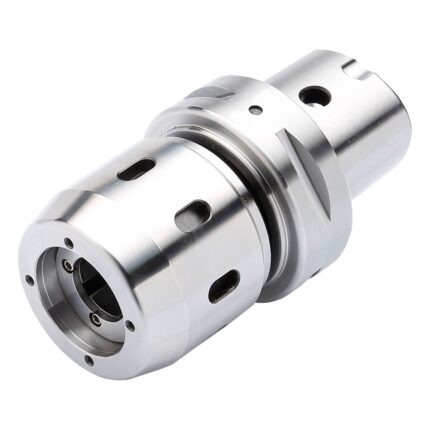
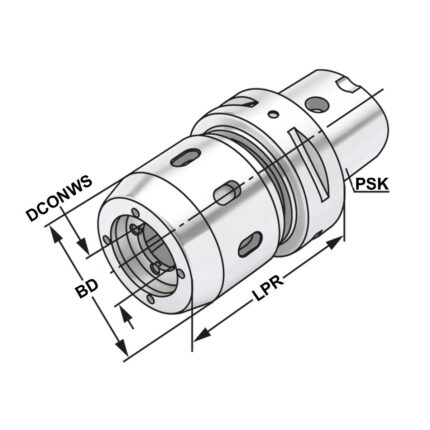
Milling Chuck PSK 63 – 32 – 85


Clamping force proofing instrument 10mm
Execution:
accurate, quick and simple measuring of the clamping force of hydraulic chucks
- mobility allows measuring within machines and fixtures
- determines clamping force via a pressure sensitive plug gauge
- display of absolute measuring value or percentage clamping force in relation to reference value

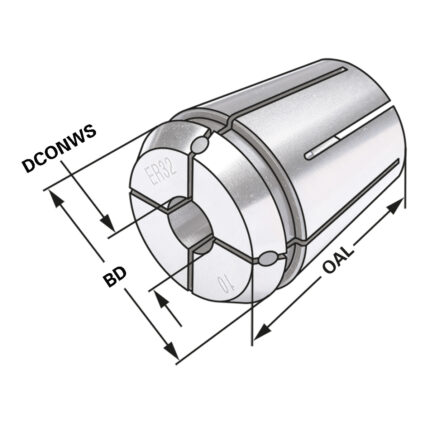
ER-Collet with seal for IC ER20 | 428EA | < 15µm | O 3
Application:
Collets sealed with seal for IC DIN 6499 B (ISO 15488 B) ER-system
Note:
Only nominal size d can be clamped with sealing plug for internal cooling (applicable up to 21 bar) In order to achieve an optimum sealing the tool must be clamped on the complete length of the ground drill of the collet.
FREE CONSULTATION
Have questions?
Leave a request
OUR PARTNERS