
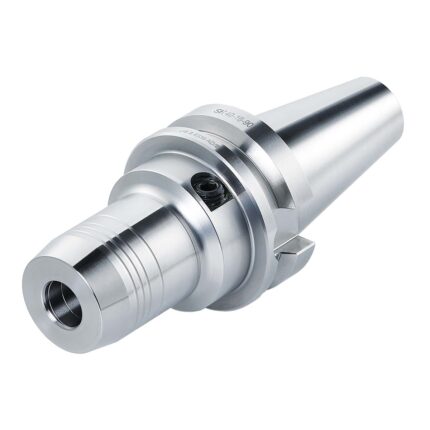

Hydraulic expansion chuck BT 30 – 20 – 90
Application:
For mounting straight-shank tools acc. DIN 1835 form A+B+E and DIN 6535 form HA+HB+HE (larger than dia. 20 mm only with reduction sleeve).
Note:
l1 = max. clamping depth l2 = max. length adjustment range
Delivery:
With wrench
- All holders are made of forged steel
- Specific, low warpage hardened
- Surface hardened HRC 58~60
- Hardening depth 0,8mm~0,9mm
- Taper angle tolerance < AT 3 according to DIN 2080
- Surface roughness Ra < 0,4 µm
- Tensile strength in the core of min. 800 N/mm? after DIN
- All functional surfaces fine machined


Morse taper adaptor SK 40 – 2 – 50
Application:
For clamping tools with Morse taper shank and thread according to DIN 228-1 form A.
Delivery:
With built-in tightening bolt
- All holders are made of forged steel
- Specific, low warpage hardened
- Surface hardened HRC 58~60
- Hardening depth 0,8mm~0,9mm
- Taper angle tolerance < AT 3 according to DIN 2080
- Surface roughness Ra < 0,4 µm
- Tensile strength in the core of min. 800 N/mm? after DIN
- All functional surfaces fine machined


Digital Caliper | 0-150mm IP67 | reading 0,01mm
Construction:
- Resolution: .0005" / 0.01mm
- Conforms to the IP67 ratings
- Extra large LCD readout
- Inch/Metric conversion
- The design allows the caliper to be used in normal workshop conditions and is resistant to coolant, water, dust or oil
- Automatic switch off
Delivery:
- Warranty card
- Instruction manual
- Calibration certificate
- CR2032 3,0V Battery
- Screwdriver
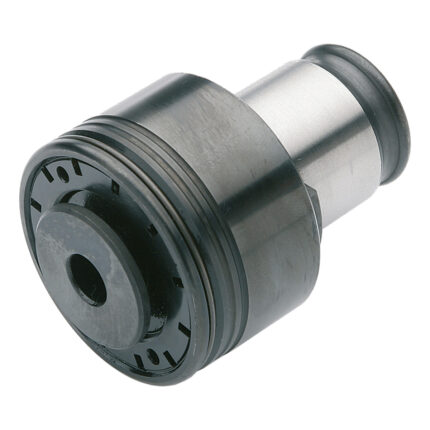

Quick change adaptors with safety clutch Size 3 | M18 | 14 x 11 | DIN 376


Collets set | 5 µm | ER40 | 472EP | 23-part kit in wooden socket DIN 6499 B (ISO 15488 B)


Axial toolholder – form C1 right C1 – 50 x 32
Application:
Mainly for external machining. For face machining.
Precision coolant supply: Improves chip evacuation and decreases the risk for chip jamming, critical factors for successful deep face grooving operations. Effective from low to high coolant pressures.With high precision coolant you get improved
chip breaking, longer tool life, better process security and productivity. Improves chip evacuation and decreases the risk for chip jamming, critical factors for successful deep face grooving operations. Effective from low to high coolant pressures.
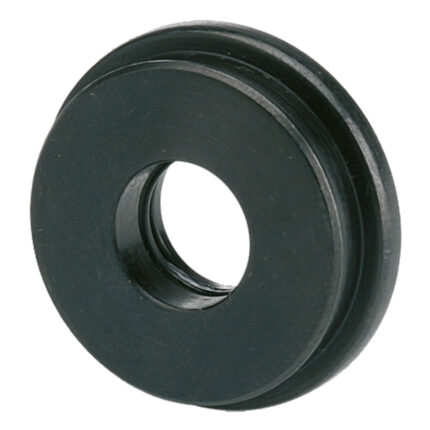
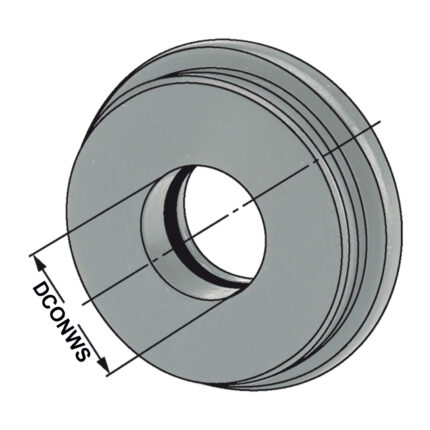
Sealing disc | ER 32 DCONWS = 8,5


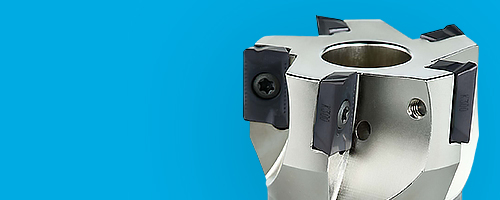
Shell mill holder BT 40 – 32 – 50
Application:
For mounting milling cutters with transversal groove.
Note:
d = 40/d = 60: For large diameter face mill cutters with four additional threaded holes according to DIN 2079.
SK 30 without coolant exit bores on the end face
Delivery:
With drivers, cross head retaining screw and cylinder head retaining screw for cutters with central coolant. For d = 60 only with four fi xation screws according to DIN 912.
- All holders are made of forged steel
- Specific, low warpage hardened
- Surface hardened HRC 58~60
- Hardening depth 0,8mm~0,9mm
- Taper angle tolerance < AT 3 according to DIN 2080
- Surface roughness Ra < 0,4 µm
- Tensile strength in the core of min. 800 N/mm? after DIN
- All functional surfaces fine machined
Have questions?
Leave a request
OUR PARTNERS