

ER-Precision collet chuck BT 30 – 2/20 – 70 ER32
Application:
For mounting straight-shank tools in 2 µm-collets.
Advantage:
- Excellent concentricity in the system (chuck + collet + clamping nut)
- 3 µm radial run-out with a 2 µm clamping nut, 6 µm radial run-out with a 5 µm clamping nut
- Extremely strong holding force (increases the holding power by at least 60% compared to standard ER chuck)
- Plain clamping nut without grooves for high speed machining


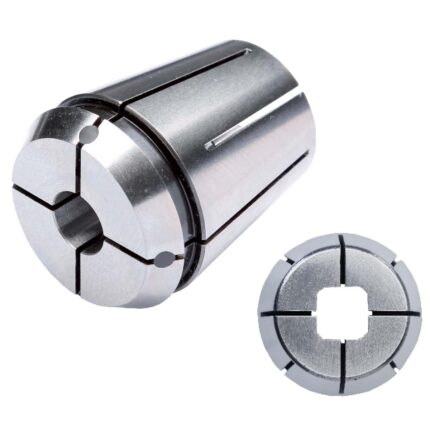
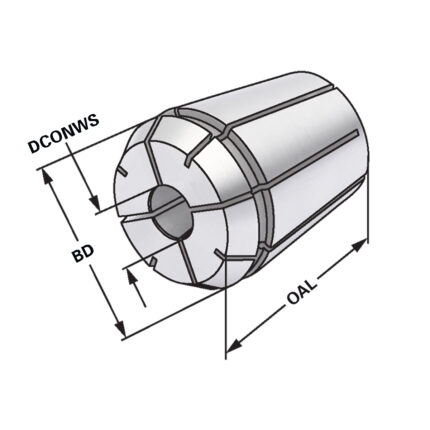
ER-Collet with seal for IC ER32 | 470EA | < 15µm | O 17
Application:
Collets sealed with seal for IC DIN 6499 B (ISO 15488 B) ER-system
Note:
Only nominal size d can be clamped with sealing plug for internal cooling (applicable up to 21 bar) In order to achieve an optimum sealing the tool must be clamped on the complete length of the ground drill of the collet.


HSSE twist drill 135° 5,6 mm DIN 338 | TIN coating
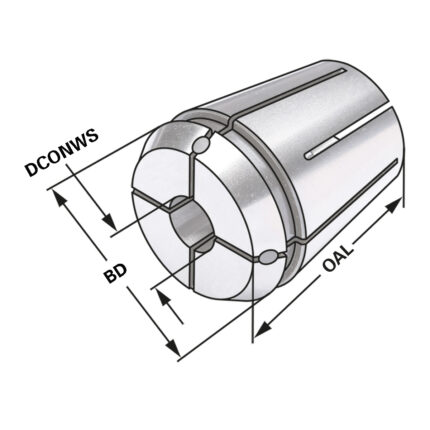
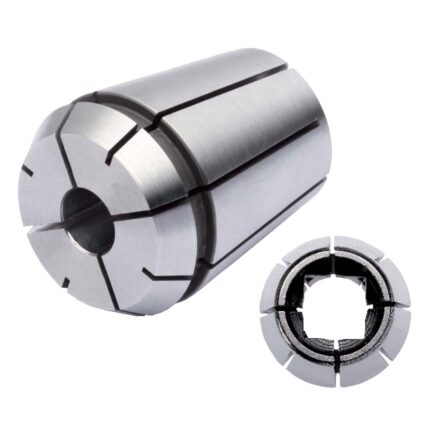
ER-Gewindebohrer-Spannzange IK ER25 | 430GA | < 15µm | 4 x 3


Radial toolholder – form B3 overhead right short B3 – 30 x 20 x 40
Application:
Mainly for external machining. For face machining.
Precision coolant supply: Improves chip evacuation and decreases the risk for chip jamming, critical factors for successful deep face grooving operations. Effective from low to high coolant pressures.With high precision coolant you get improved
chip breaking, longer tool life, better process security and productivity. Improves chip evacuation and decreases the risk for chip jamming, critical factors for successful deep face grooving operations. Effective from low to high coolant pressures.


Milling arbors for screw-in cutters SK 40 – M6 – 69 – LB50
Application:
For mounting screw-in cutters with thread.
- All holders are made of forged steel
- Specific, low warpage hardened
- Surface hardened HRC 58~60
- Hardening depth 0,8mm~0,9mm
- Taper angle tolerance < AT 3 according to DIN 2080
- Surface roughness Ra < 0,4 µm
- Tensile strength in the core of min. 800 N/mm? after DIN
- All functional surfaces fine machined
Have questions?
Leave a request
OUR PARTNERS