

HSS-E spiral flute taps M6 6×4,9 P=1,0
Application:
- Thread configuration with a special design, prevents overfeeding, thin thread and pitch diameter oversize.
- Flute geometry with special design, better chip evacuation, prevents chip clogging, improves thread quality
- Excellent performance on various work material: Stainless steel, carbon steel, alloyed steel, tool steel
Hydraulic expansion chuck SK 50-32-91 DIN 69871 AD/B in wooden box
Application:
For mounting straight-shank tools acc. DIN 1835 form A+B+E and DIN 6535 form HA+HB+HE (larger than dia. 20 mm only with reduction sleeve).
Note:
l1 = max. clamping depth l2 = max. length adjustment range
Delivery:
With wrench
- All holders are made of forged steel
- Specific, low warpage hardened
- Surface hardened HRC 58~60
- Hardening depth 0,8mm~0,9mm
- Taper angle tolerance < AT 3 according to DIN 2080
- Surface roughness Ra < 0,4 µm
- Tensile strength in the core of min. 800 N/mm? after DIN
- All functional surfaces fine machined


ER-Collet chuck HSK 63 – 2/13 – 200 | ER 20
Application:
For mounting straight-shank tools in collets.
Delivery:
With balanced clamping nut
- All holders are made of forged steel
- Specific, low warpage hardened
- Surface hardened HRC 58~60
- Hardening depth 0,8mm~0,9mm
- Taper angle tolerance < AT 3 according to DIN 2080
- Surface roughness Ra < 0,4 µm
- Tensile strength in the core of min. 800 N/mm? after DIN
- All functional surfaces fine machined


Shell mill holder SK 40 – 32 – 130
Application:
For mounting milling cutters with transversal groove.
Note:
d = 40/d = 60: For large diameter face mill cutters with four additional threaded holes according to DIN 2079.
SK 30 without coolant exit bores on the end face
Delivery:
With drivers, cross head retaining screw and cylinder head retaining screw for cutters with central coolant. For d = 60 only with four fi xation screws according to DIN 912.
- All holders are made of forged steel
- Specific, low warpage hardened
- Surface hardened HRC 58~60
- Hardening depth 0,8mm~0,9mm
- Taper angle tolerance < AT 3 according to DIN 2080
- Surface roughness Ra < 0,4 µm
- Tensile strength in the core of min. 800 N/mm? after DIN
- All functional surfaces fine machined


ER-Precision collet ER16 | 426EP | < 5µm | O 10 - 9
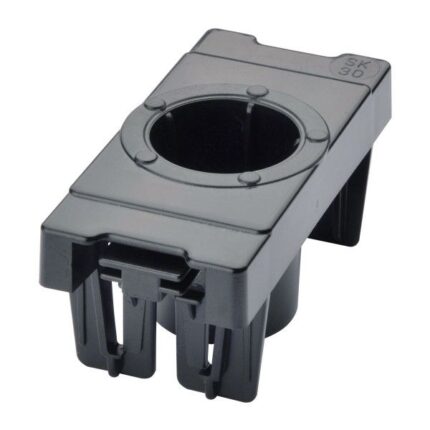
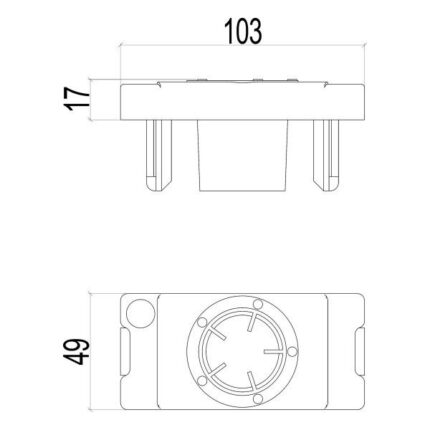
CNC Werkzeugeinsatze | Typ 2 MK 4
The tool inserts are made of oil-resistant,
break-proof and impact-resistant ABS plastic
and are noted for their tailored inner struts.
The tapered tool holder is thus optimally
centred.
The insert is clicked into our grid system with
a clip and can be moved in steps of 25 mm
without a tool.
Nubs on the top of the inserts.
In this way, no adhesion occurs and the tool
is prevented from attaching itself by vacuum
All tool sizes can be combined
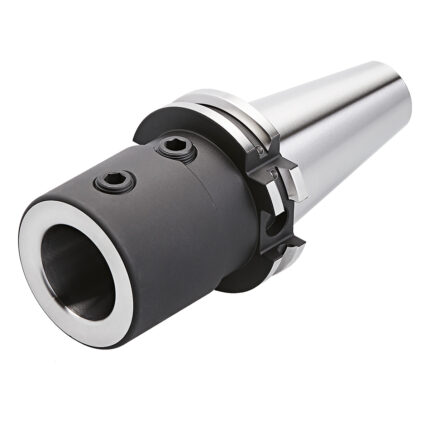
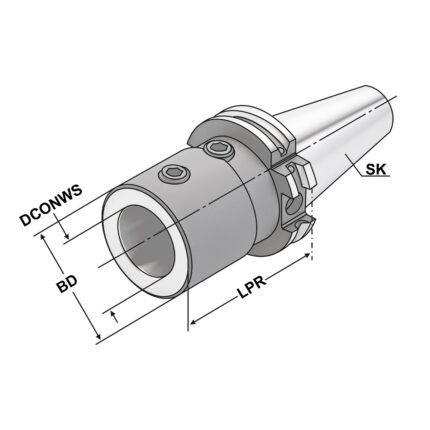
Boring holder for drills with indexable inserts | SK 40 – 25 – 70
Application:
For mounting solid drills with cylindrical shank according to DIN 6595.
Note:
Contact surface precision grinded
Delivery:
With clamping screws
- All holders are made of forged steel
- Specific, low warpage hardened
- Surface hardened HRC 58~60
- Hardening depth 0,8mm~0,9mm
- Taper angle tolerance < AT 3 according to DIN 2080
- Surface roughness Ra < 0,4 µm
- Tensile strength in the core of min. 800 N/mm? after DIN
- All functional surfaces fine machined
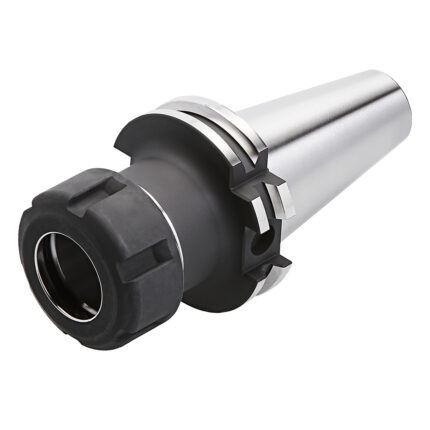
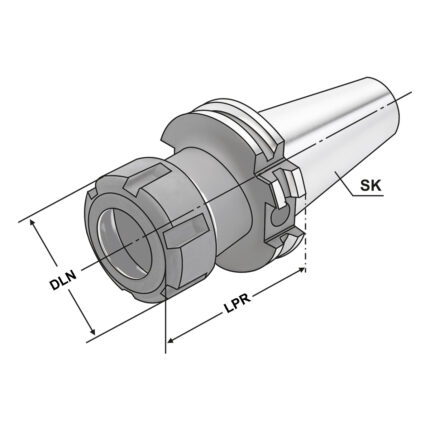
ER-Collet chuck SK 40 – 2/16 – 100 | ER 25
Application:
For mounting straight-shank tools in collets.
Delivery:
With balanced clamping nut
- All holders are made of forged steel
- Specific, low warpage hardened
- Surface hardened HRC 58~60
- Hardening depth 0,8mm~0,9mm
- Taper angle tolerance < AT 3 according to DIN 2080
- Surface roughness Ra < 0,4 µm
- Tensile strength in the core of min. 800 N/mm? after DIN
- All functional surfaces fine machined
Have questions?
Leave a request
OUR PARTNERS